Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM


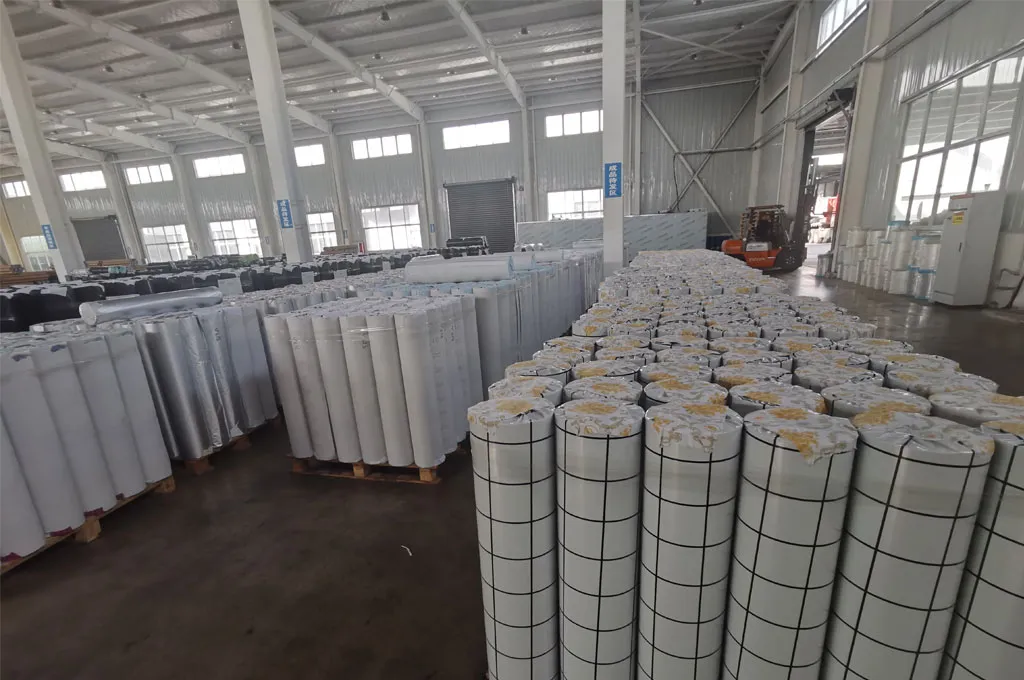
Export rejections for PVC film can be costly and time-consuming. Buyers, customs inspectors, and freight handlers commonly reject shipments due to quality, documentation, or packaging issues. This guide explains the most frequent causes of rejection and gives practical, export-ready steps to avoid them so your shipments clear quickly and consistently.
What happens: Customs labs or importers test for prohibited plasticizers, heavy metals, or additives. If results exceed the destination country’s limits, the shipment can be detained or destroyed.
How to avoid: Use certified raw materials, obtain third-party test reports (RoHS, REACH, phthalate-free certificates) and include these documents with shipping papers.
Issues like inconsistent thickness, pinholes, delamination, or surface contamination lead to outright rejection by OEMs and distributors. Small defects scale into large complaints when many rolls are affected.
Preventive measures: implement tight in-line quality control (thickness gauges, visual inspection) and keep batch records so you can trace and isolate problems quickly.
Common administrative reasons for rejection include missing commercial invoices, packing lists, material safety data sheets (MSDS), or incorrect HS codes. Import regulators are strict: paperwork errors often stop clearance.
Solution: use a standardized export document checklist and cross-check HS codes and product descriptions with the buyer before booking transport.
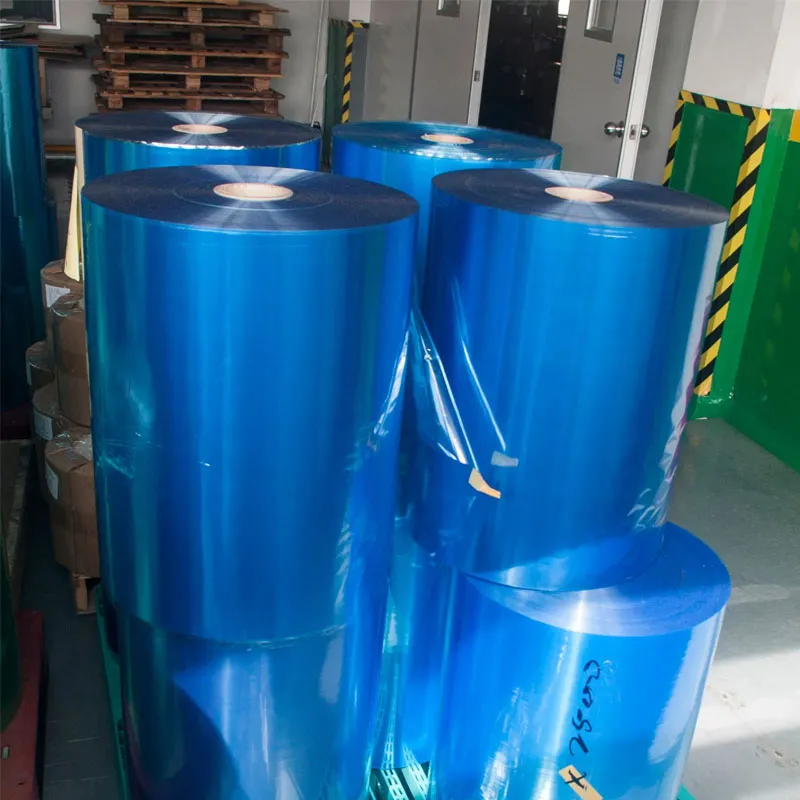
Film rolls moved internationally must resist moisture, abrasion, and pressure. Rejection reasons include water damage, crushed ends, or contaminated outer wraps. Proper protective packaging prevents physical and reputational loss.
Best practice: individually wrap rolls in dust-proof PE or kraft paper, use end caps, palletize with shrink wrap, and mark cartons with handling instructions.
If the film or its packaging contains chemicals that require hazard classification under international transport rules (IMDG, IATA), missing or wrong markings cause shipment blocks.
Fix: consult transport regulations early, provide accurate GHS labels, and ensure carriers are informed about any regulated components.
Especially for decorative or laminated PVC films, color tolerance and print registration issues are reasons for buyer rejection. Even small variances can be unacceptable for retail or OEM applications.
How to reduce risk: approve final color proofs, record supplier color standards, and perform batch color checks against approved samples.
| Issue | Root Cause | Action to Take |
|---|---|---|
| Chemical non-compliance | Unverified additives or plasticizers | Require supplier COA & lab test before shipment |
| Surface defects | Contamination or poor calendering control | Use inline QC & cleanroom protocols for finishing |
| Documentation gaps | Missing MSDS/HS code mismatch | Standardize export paperwork template |
| Packaging damage | Insufficient protection or palletizing | Adopt roll-by-roll wrapping and pallet straps |
EU importers focus on REACH, RoHS, and strict labeling. Provide test certificates and material declarations up front.
Regulatory scrutiny varies but packing integrity and clear invoices reduce customs delays. Local buyers often expect IEC or regional test evidence for electrical or flame-retardant films.
Pulivk — vertically integrated production with calendering, printing, and split-packaging lines helps control material sources, quality, and lead times to reduce export risk.
Consistency is the best defense against export rejection. Standardize QC, document everything, and align with buyers on acceptance criteria before production starts. That approach saves time, reduces cost, and builds strong export performance.