Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM


PVC film production lines combine precise mechanical systems, temperature control, and finishing equipment to convert raw PVC compounds into decorative and protective films used across flooring, furniture, kitchen, automotive, and packaging industries. This guide breaks down the essential components, the typical process flow, operational specs, and practical tips to optimize performance and product quality.
Understanding each component helps manufacturers select the right configuration for product types such as glossy film, wood grain film, marble film, anti-oil kitchen film, and adhesive-backed films. Below is a concise list of the core equipment on most calendered PVC film lines.
The extruder melts and homogenizes the PVC compound. Typical options include single-screw or twin-screw extruders depending on throughput and additive mixing needs. A stable feeding system and gravimetric feeders ensure consistent melt viscosity and color distribution.
A calender roll stack (often 3 to 5 rollers) determines film thickness and surface finish. Precision temperature control across heated rolls creates consistent gloss, emboss patterns, and thickness tolerances. Roll surface treatments (chrome, ceramic) affect final texture and wear resistance.
Chill rolls rapidly cool the extruded film to lock in surface patterns and dimensional stability. Efficient water circulation and independent temperature zones are critical for high-speed production.
Embossing rollers imprint wood grain, cloth grain, stone textures, or 3D relief patterns. For multi-layer composite films, synchronized embossing ensures alignment across layers.
Gravure or flexographic printing units apply decorative patterns and protective coatings. UV or solvent-based coatings add scratch resistance, anti-skid, or anti-fingerprint properties. Inline printing improves registration and reduces handling.
Laminators are used to bond decorative PVC to carrier substrates (paper, non-woven, or PET) or to add release liners for self-adhesive films. Controlled nip pressure and web tension prevent delamination and wrinkling.
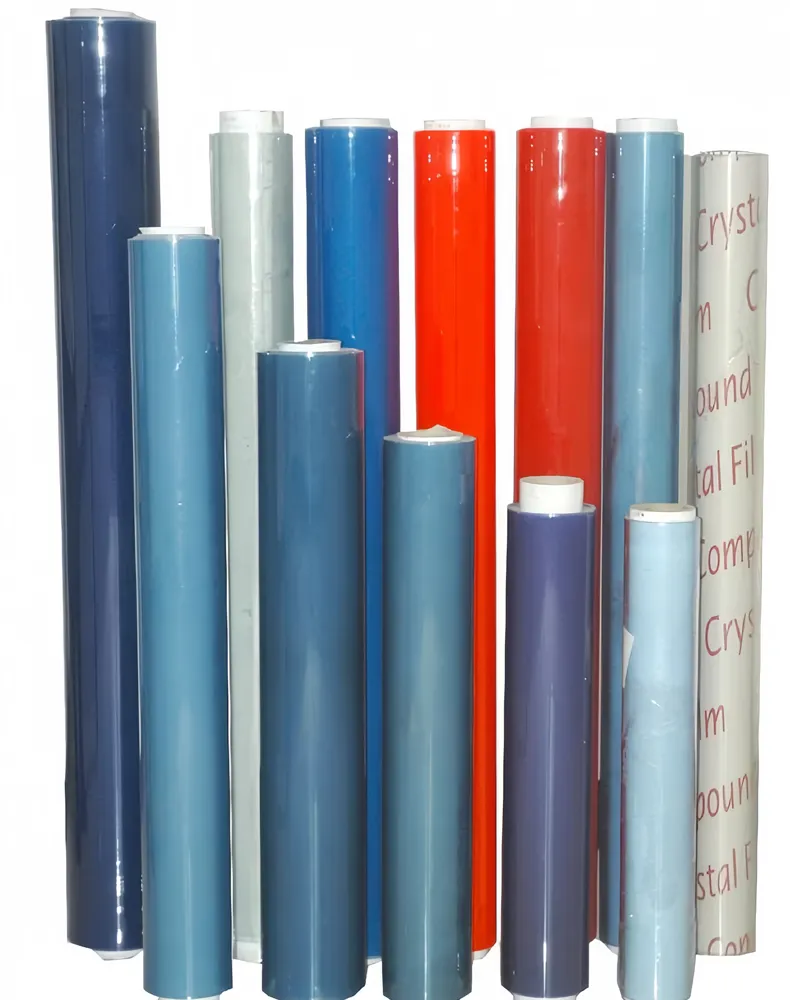
Automated slitting heads and rewinding units convert jumbo rolls into customer-specific widths and lengths. Split-packaging lines cut and package rolls to fixed lengths, wrap each roll in dust-proof PE or kraft paper, and label for shipment.
Online thickness gauges, gloss meters, and defect detection cameras help maintain production standards. Multiple QC checkpoints—raw material inspection, inline checks, and final roll testing—are recommended for consistent output.
From compound to finished roll, a streamlined PVC film line follows these stages:
Blend PVC resin, plasticizers, stabilizers, pigments, and additives in mixers. Use gravimetric feeders to maintain consistent formulation.
Extrude melt through the die onto the calender stack. Adjust roll gaps and temperatures to achieve target thickness (commonly 0.02–1.2 mm for decorative films).
Cool the web with chill rolls; emboss patterns while the film is still warm for better texture fidelity.
Apply surface graphics or protective coatings. Drying sections and UV curing stations follow printing areas.
Cut to width, rewind under controlled tension, and send to split-packaging. Labeling ensures traceability for export and OEM orders.
| Component | Primary Function | Key Specs / Notes |
|---|---|---|
| Extruder | Melting & mixing | Throughput 200–1500 kg/h; twin-screw for additives |
| Calender Stack | Thickness & surface finish | 3–5-roll; temperature control ±1°C |
| Embossing Rolls | Texture & pattern | Custom chrome/copper cylinders; registration control |
| Printing Unit | Decorative patterns | Flexo/gravure; in-line UV curing |
| Slitter & Rewinder | Convert to finished rolls | Cutter types: razor / shear; tension control |
Calendered PVC film lines vary by investment and product mix. Typical running speeds: 10–60 m/min. Thickness ranges from 20 µm for protective overlays up to 1.2 mm for flooring films. Common widths: 1220 mm, 1400 mm, 2000 mm, and custom widths for OEM orders.
Consistent QC is essential. Monitor melt temperature, roll temperature, web tension, and coating cure levels. Address these common issues:
Check roll parallelism, die lip adjustment, and gravimetric feed stability.
Inspect raw material blending and degassing on the extruder; verify roll surface finish and cleaning schedule.
Review bonding adhesive, temperature profile, and nip pressure in laminating stations.
Manufacturers often require tailored thicknesses, print patterns, adhesion properties, and packaging. A vertically integrated supplier that controls calendering, printing, and split-packaging can shorten lead times and reduce cost variation. For international buyers, ensure proper labeling, palletization, and export paperwork for smooth logistics.
Regular preventive maintenance keeps yields high. Key items include roll surface inspections, hydraulic checks, gearbox lubrication, and calibration of inline gauges. Implement safety guards around nip points, lockout-tagout procedures for roll changes, and employee training for solvent/UV operations.
Producers that manage compounding, calendering, printing, and packaging under one roof gain better quality control, lower procurement complexities, and improved responsiveness to OEM demands. Companies offering these capabilities can support global markets with consistent product specs and steady lead times—helping partners reduce costs at the source. Pulivk provides this integrated approach through in-house calendering, printing, and split-packaging lines.
If you are evaluating PVC film suppliers or planning a new product line, gather target thickness, width, pattern type, and annual volume. These details will determine the optimal production configuration, tooling, and expected lead times.