Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM


 ByPulivk
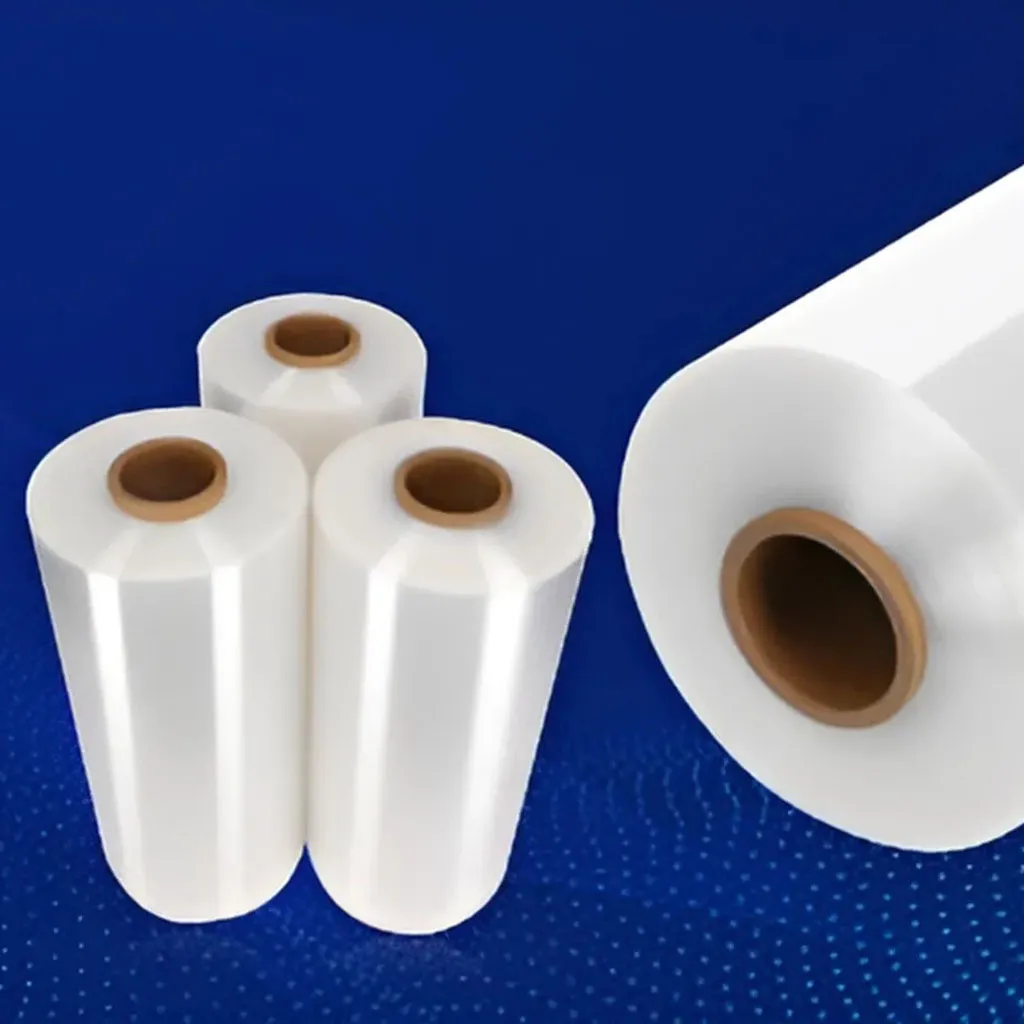
Vacuum packaging film is a high-barrier plastic material designed to remove air and form a tight, protective envelope around products. Used across food, medical, industrial, and electronic packaging, these films block oxygen, moisture, and contaminants to extend shelf life and preserve quality.
In simple terms, vacuum packaging film is a flexible polymer sheet engineered for vacuum-sealing processes. Typical constructions include multi-layer laminates combining materials such as polyamide (PA), polyethylene (PE), polyester (PET), and barrier layers like EVOH or PVDC. These combinations deliver the strength, puncture resistance, and gas-barrier performance required for effective vacuum packaging.
Polyamide (PA) — provides puncture and abrasion resistance for sharp or heavy foods.
Polyethylene (PE) — offers sealability and flexibility for reliable heat seals.
EVOH / PVDC — high oxygen barriers used when long shelf life is essential.
PET / Metallized layers — add strength, heat resistance, and optional gas/light blocking.
Films range from simple mono-layer PE for basic vacuum pouches to sophisticated 5–7-layer laminates for frozen meat, cheese, and ready meals. Choosing the right structure depends on product sensitivity, intended shelf life, and sealing equipment.
Vacuum packaging films are versatile and widely used in:
Food packaging — meat, seafood, cheese, coffee, nuts, and cooked meals where oxygen control prevents oxidation and microbial growth.
Medical and pharmaceutical — sterile barrier protection for instruments and devices.
Electronics and components — moisture and dust protection during storage and shipping.
Industrial parts — corrosion prevention for metal parts and long-term storage of precision components.
Shelf life extension, improved appearance, reduced food waste, and safer transport are the primary advantages. Vacuum film also supports attractive retail presentation by reducing drip and preserving color and aroma.
The following table summarizes typical film types and expected shelf-life improvements under vacuum packaging conditions. Actual results depend on product, storage temperature, and processing.
| Film Type | Typical Layers | Best For | Shelf-Life Improvement |
|---|---|---|---|
| PA/PE Laminate | PA | Tie | PE | Fresh meat, deli products | ~2–4× |
| EVOH Barrier Laminate | PET | EVOH | PE | Cooked meals, cheese | ~3–6× |
| Mono-PE | PE (single layer) | Simple vacuum pouches, non-sensitive items | ~1.2–2× |
Consider these criteria when selecting film:
Barrier needs — oxygen and moisture transmission targets.
Puncture resistance — for bones, sharp edges, or frozen goods.
Seal strength and temperature range — match to your vacuum sealer or MAP equipment.
Compliance — food contact approvals, medical grading where required.
Appearance — transparent vs. printed or metallized for retail appeal.
Optimize performance with a few practical steps:
Set the correct vacuum level — too low and air remains; too high may crush delicate items.
Use recommended seal temperatures and dwell time for the film type to avoid weak seals or film deformation.
Inspect for sharp edges and pack items with protective layers or trays to prevent punctures.
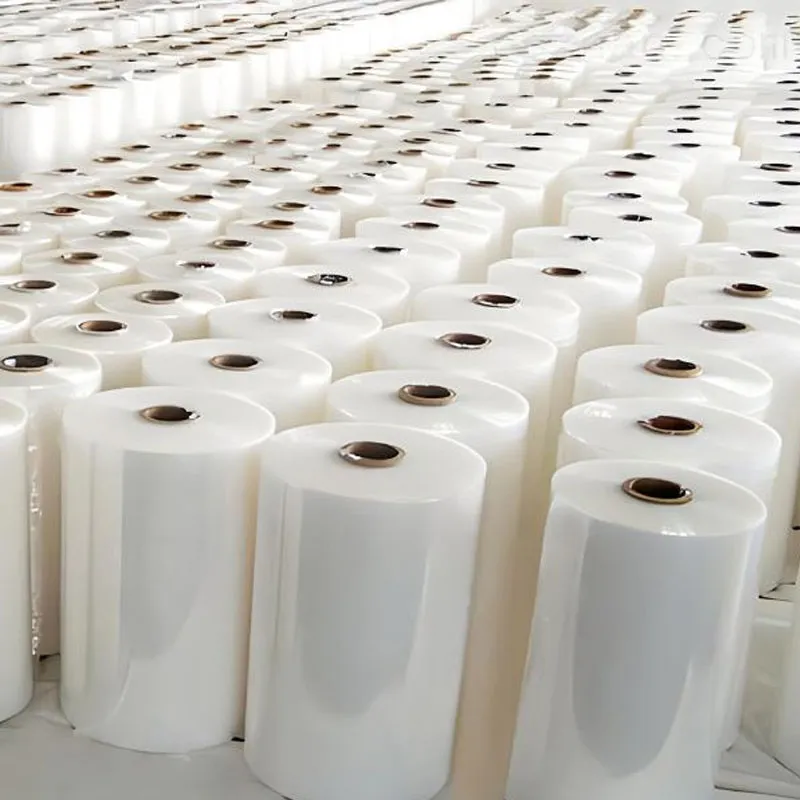
Store film rolls in a cool, dry place to preserve handling properties and sealability.
Manufacturers often offer custom sizes, printed branding, and private-label options. For example, Pulivk (https://pvcfilmtec.com/) supports tailored film constructions, printing, and split packaging to match production and retail needs.
While high-barrier laminates can be challenging to recycle, innovations and mono-material barrier options are making vacuum films more sustainable. When evaluating suppliers, consider recyclability, recyclate content, and opportunities for reduced material thickness without sacrificing performance.
Vacuum packaging film is an investment in quality preservation, waste reduction, and supply chain reliability. Selecting the right film balances cost with barrier performance, mechanical strength, and machine compatibility. With proper specification and handling, vacuum film pays back through longer shelf life, fewer returns, and stronger retail presentation.