Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal St.
Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM


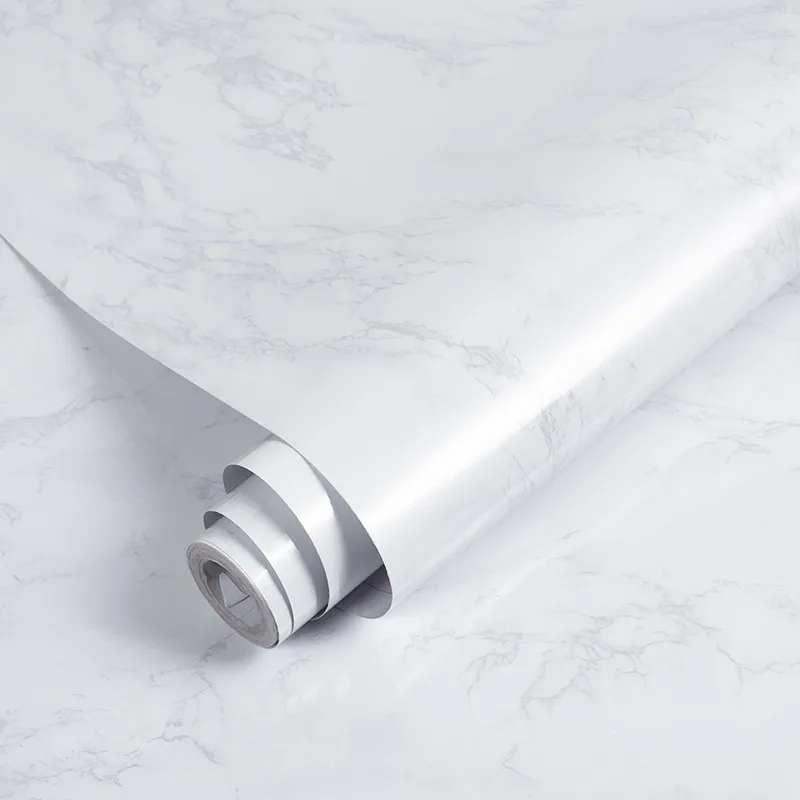
PVC film can be stamped, punched, and formed into a wide range of shapes — from simple cutouts to detailed 3D contours — using the right combination of material selection, tooling, and forming method. This guide explains when cold punching works, when heat or thermoforming is necessary, common industrial methods, and practical tips to get consistent, high-quality results.
PVC films vary by composition and process: calendered, cast, plasticized (flexible) or unplasticized (rigid) layers. These differences determine how a film responds to mechanical punching, embossing, or thermoforming:
Cold punching (mechanical die-cutting) is fast and cost-effective for flat shapes and labels. Use rotary punches, flatbed presses, or laser cutting for contours and holes. Thermoforming or heat-assisted stamping is used for shaping PVC into 3D profiles or deep grooves where material must soften and stretch.
Manufacturers typically choose from several stamping and forming techniques depending on scale and complexity:
Die cutting is ideal for flat shapes and labels. Key considerations:
Kiss cutting cuts the top film layer without cutting the backing — useful for adhesive films. Rotary scoring pre-weakens lines for easier folding and forming.
Laser cutting provides high precision and is excellent for prototypes or detailed patterns. Watch for edge discoloration and melted beads — parameters must be tuned for PVC to avoid toxic fumes; adequate ventilation and fume extraction are mandatory.
For shaping PVC film to 3D profiles, heating the film to a controlled temperature and using molds with vacuum/pressure yields smooth, consistent contours. Flexible calendered films typically require much lower forming temperatures than rigid PVC sheets.
Below is a compact reference for common film types and recommended processing choices. Values are typical starting points — always validate with sample runs.
| Film Type | Best Method | Notes |
|---|---|---|
| Flexible calendered PVC (0.05–0.5mm) | Rotary punching / Kiss cutting | Low force, good elasticity; easy for high-volume cutting |
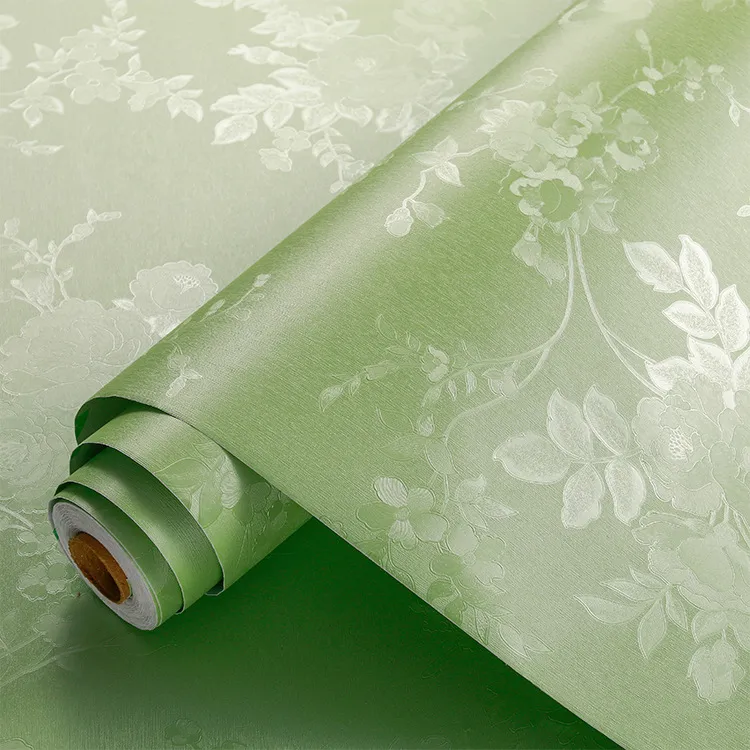
| Embossed/coated decorative films | Flat die cutting / Low-temp forming | Test for surface distortion; use supportive backing |
| Rigid PVC sheet (>0.5mm) | Thermoforming / Vacuum forming | Requires controlled heating and slow forming to avoid cracks |
Inspect edge quality, dimensional tolerance, surface gloss, and adhesion (for self-adhesive films). Run short trials and measure scrap rates before full production.
PVC processing can generate fumes under high heat; ensure proper extraction and compliant workplace controls. Consider material recycling streams and select formulations optimized for lower environmental impact where possible.
For consistent production, choose suppliers who control calendering, printing, and split-packaging in-house—this reduces variability and supports faster lead times. Pulivk (https://pvcfilmtec.com/) offers full in-house production with calendering, printing, and split-packaging lines to support OEM and custom orders.
If you need tailored advice for a specific PVC film or part geometry, run material samples with your intended tooling and consider vendor collaboration during prototyping to ensure a cost-effective, high-quality production setup.